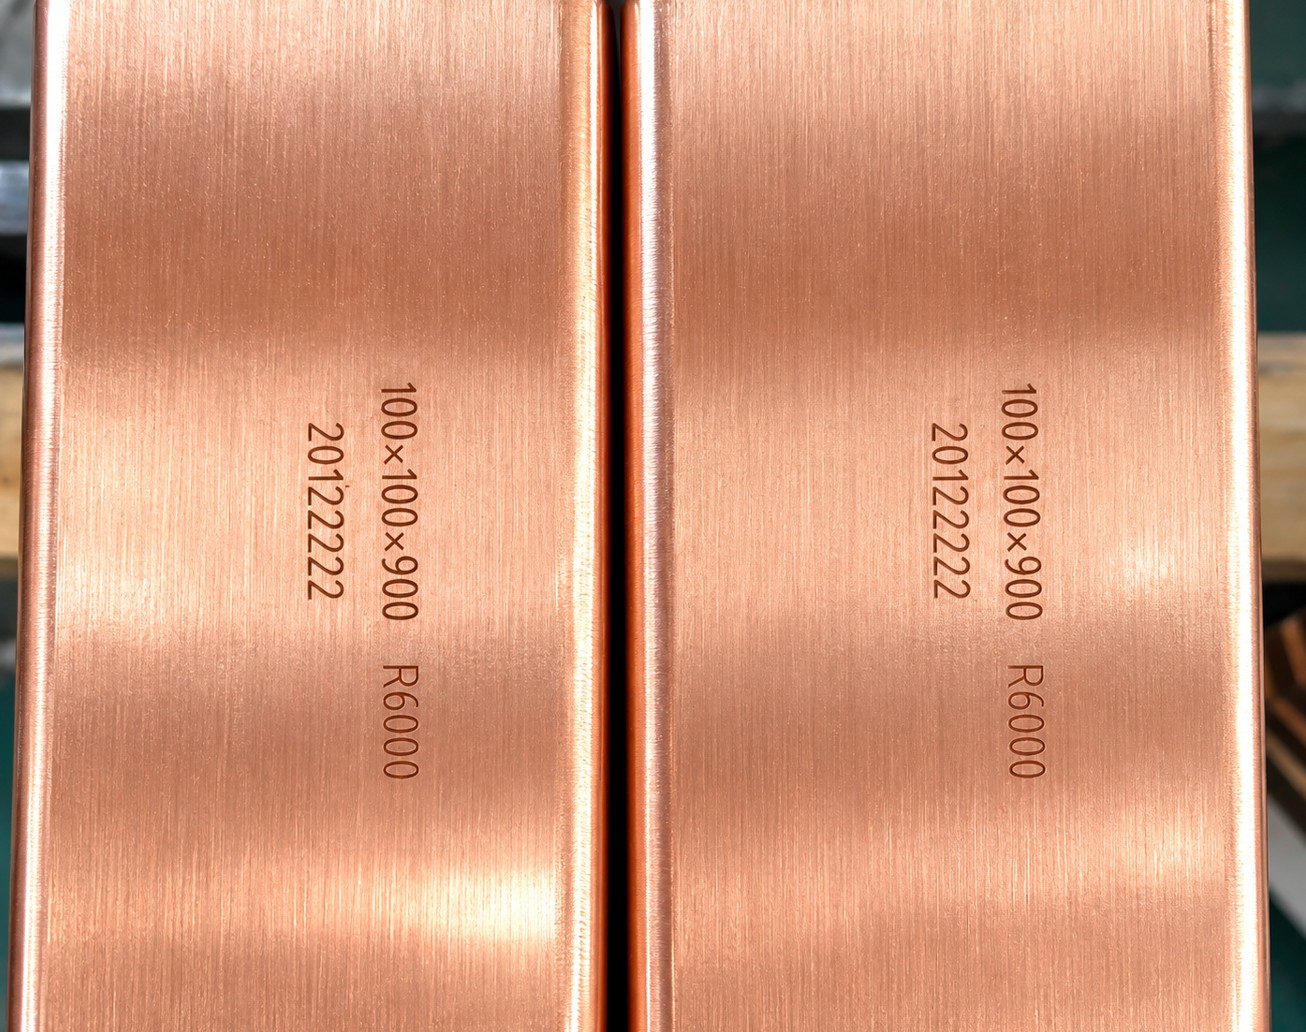
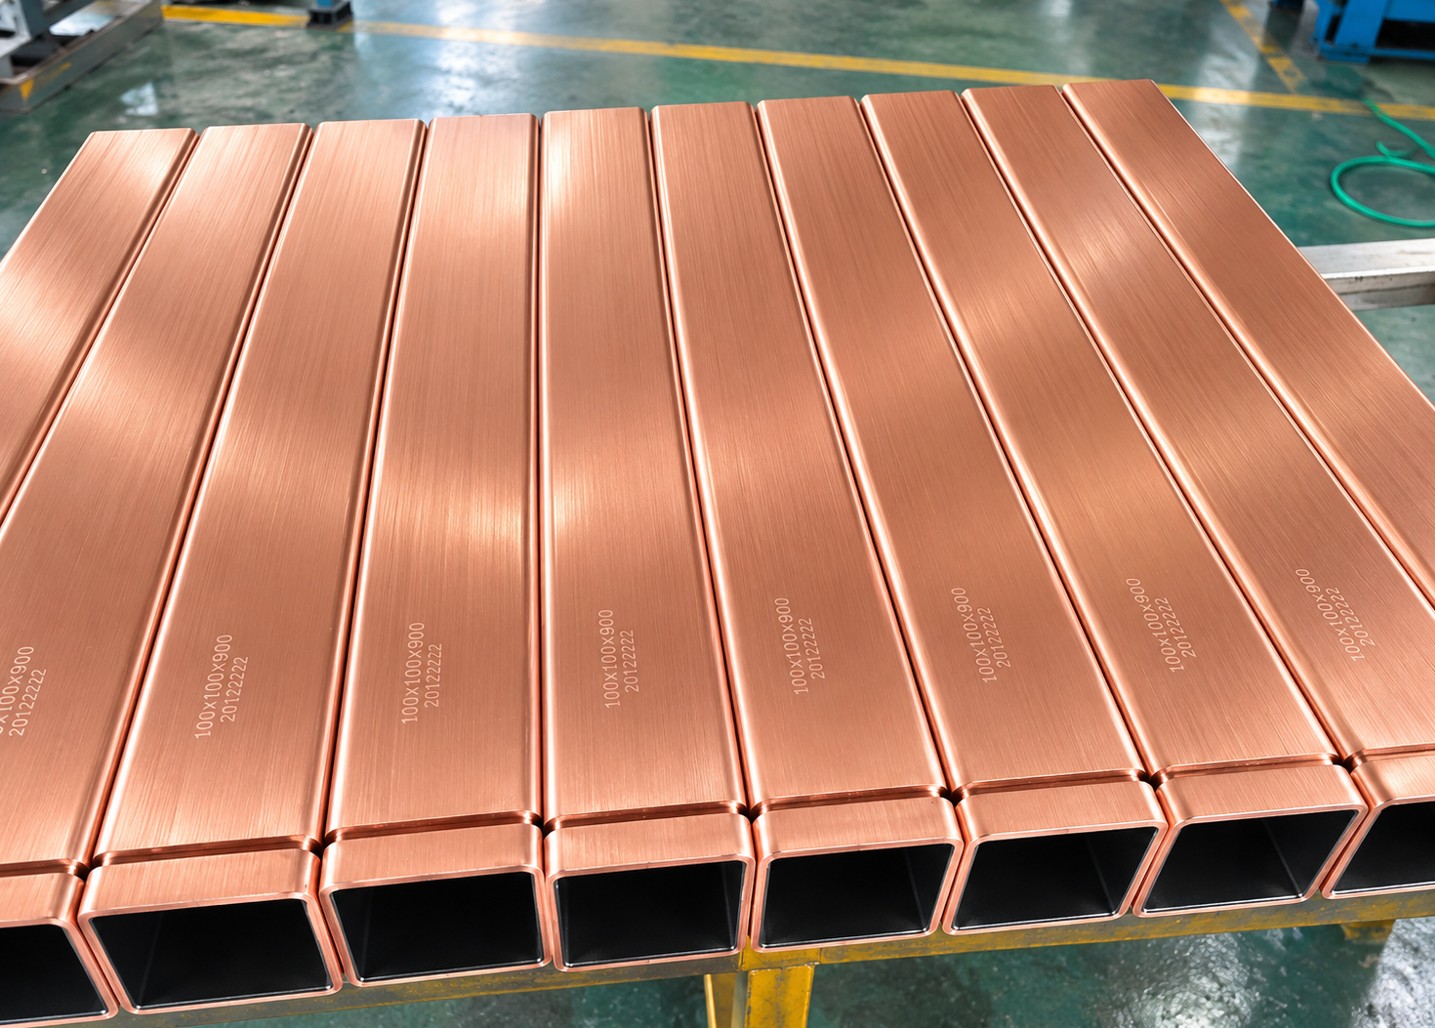
R6 100 × 100 mm
- Radius
- R6 (6000 mm)
- Section
- 100 × 100 mm
- Length
- 900 mm
- Wall
- 12 mm
- Material
- Cu-DHP / CuAg / CuCrZr
- Plating
- Hard chrome 0.08–0.12 mm
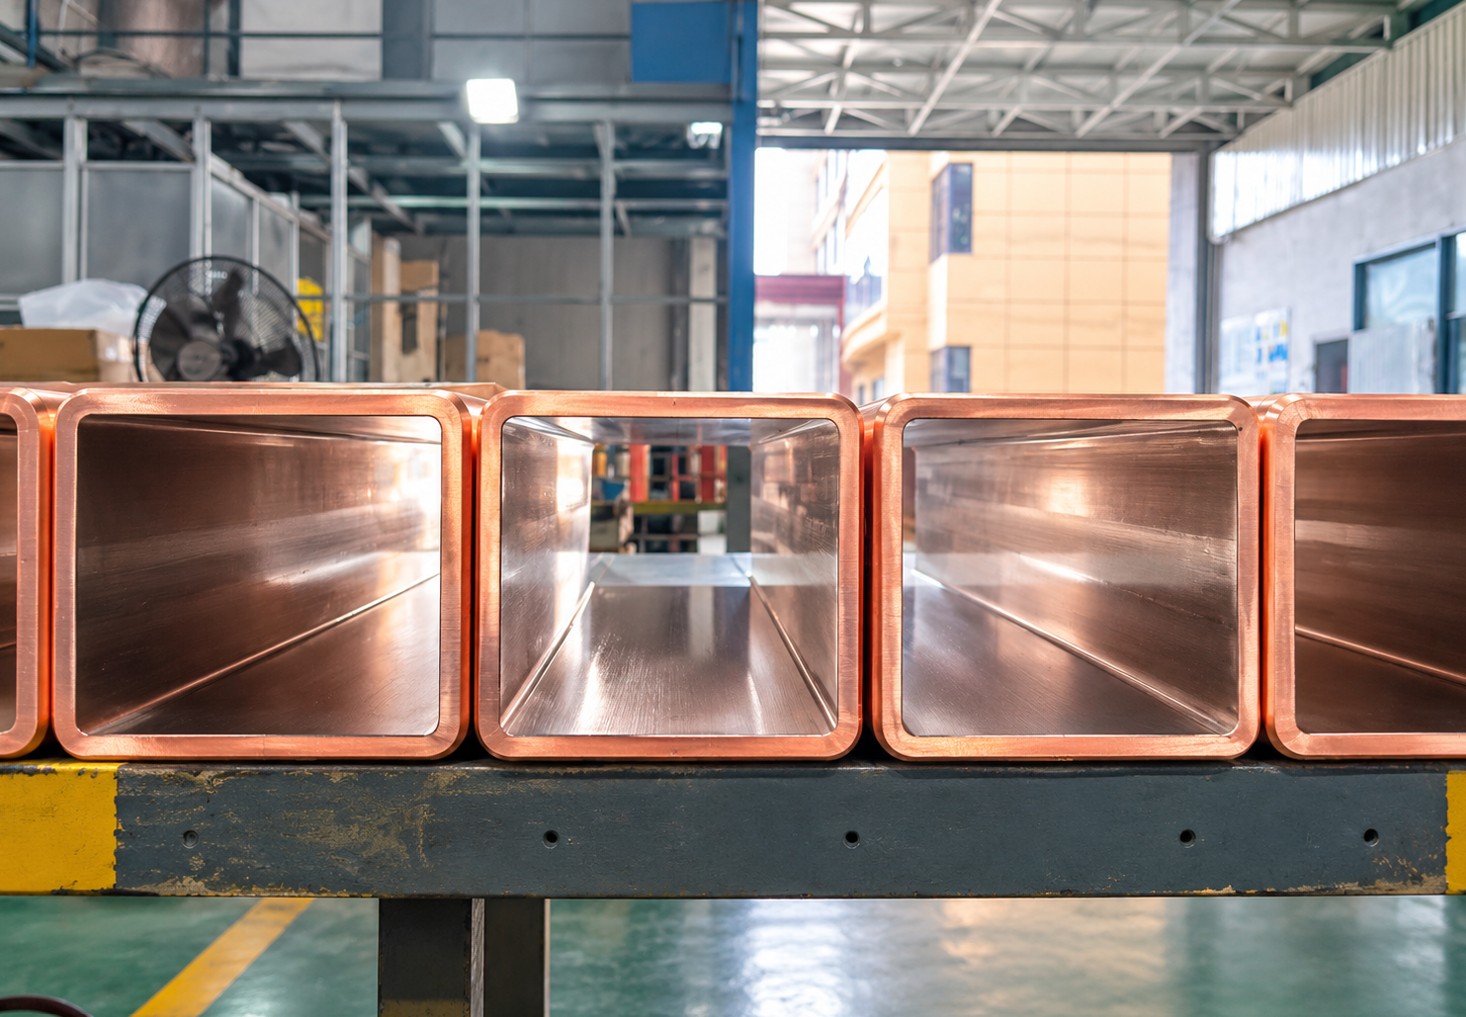
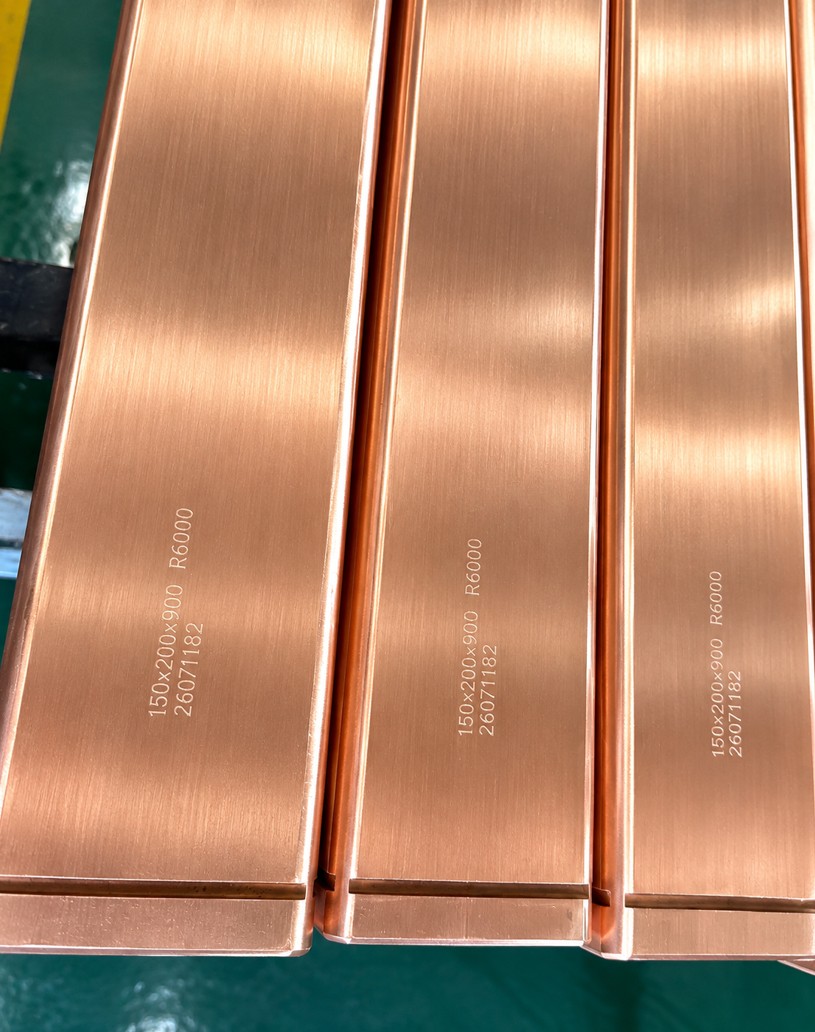
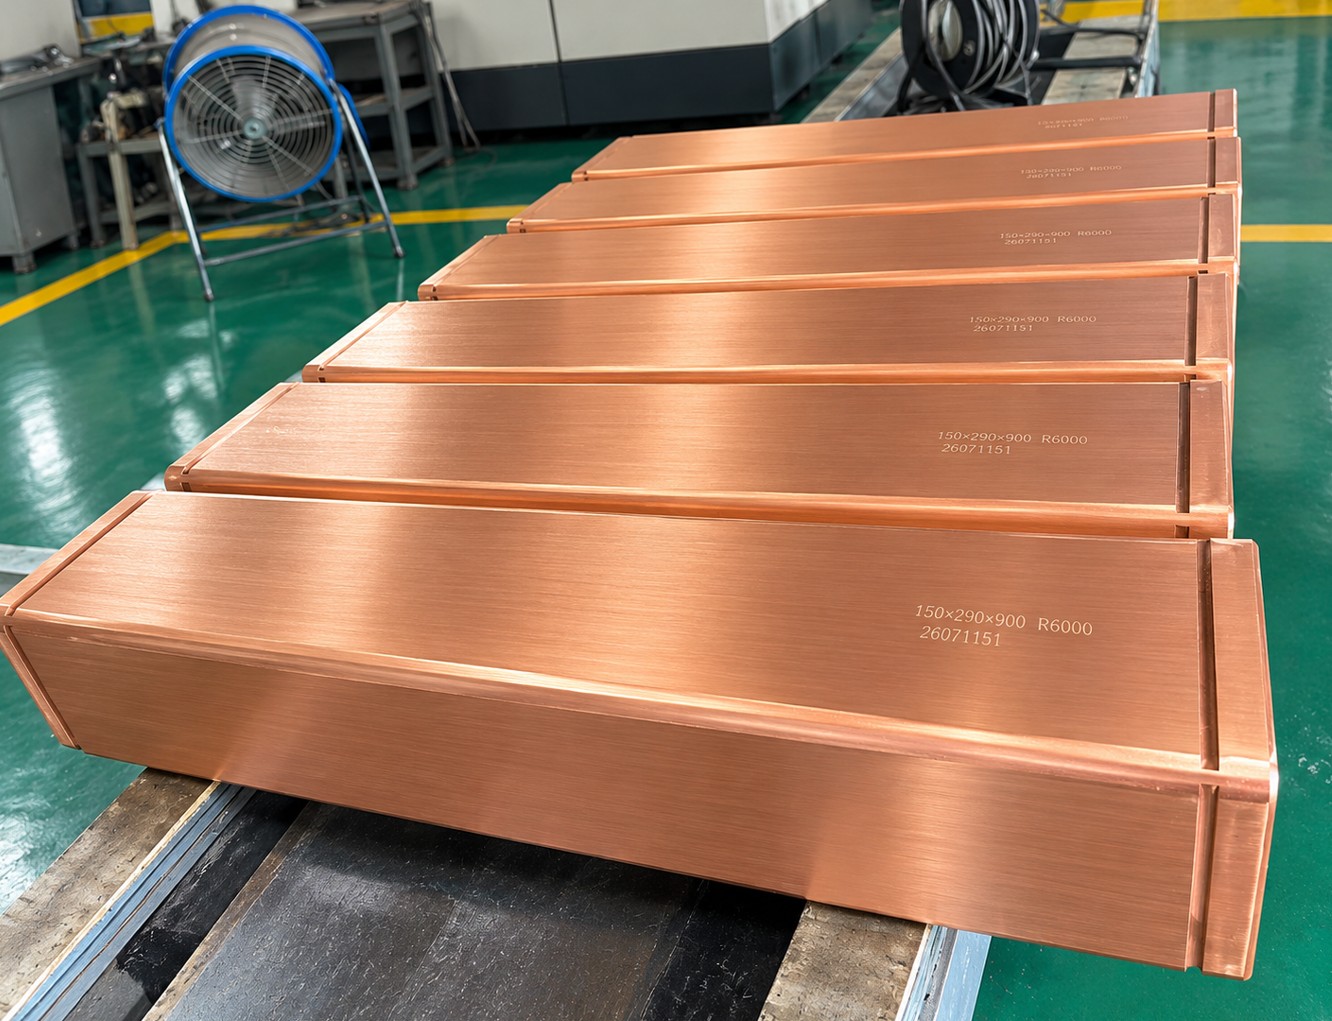
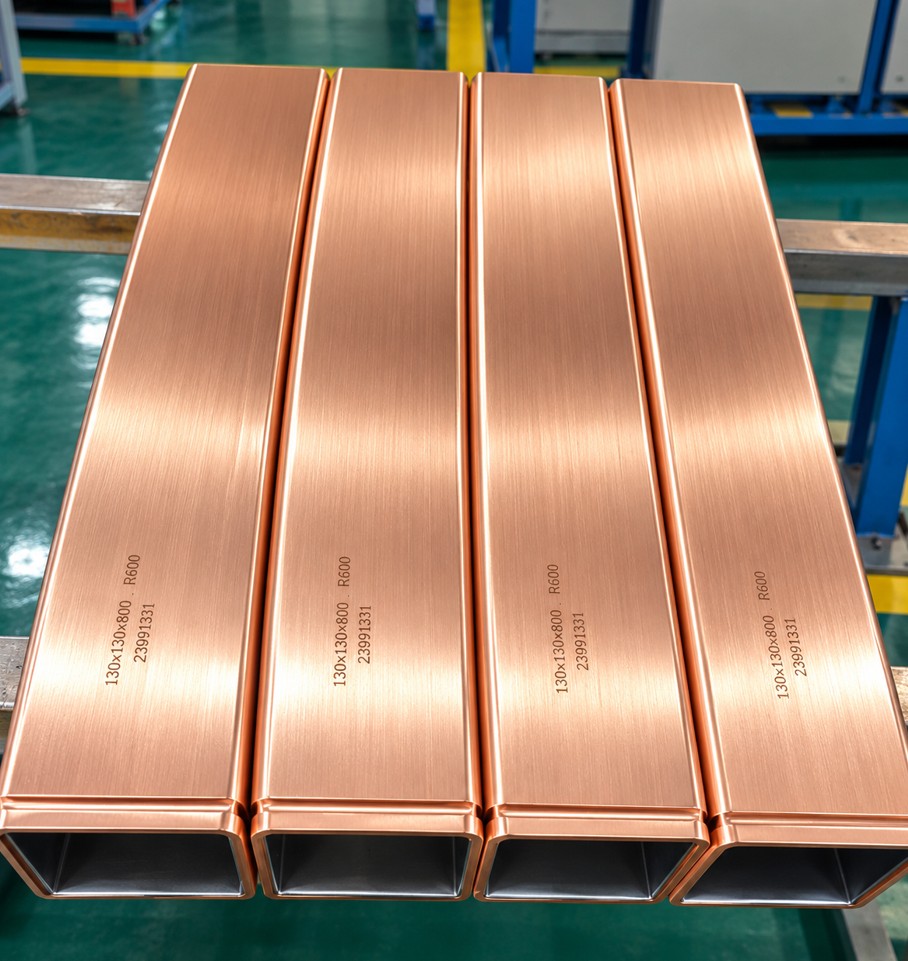
The five specifications below cover most billet casters we supply. Each is shown with the outer surface and the chrome-plated inner surface.
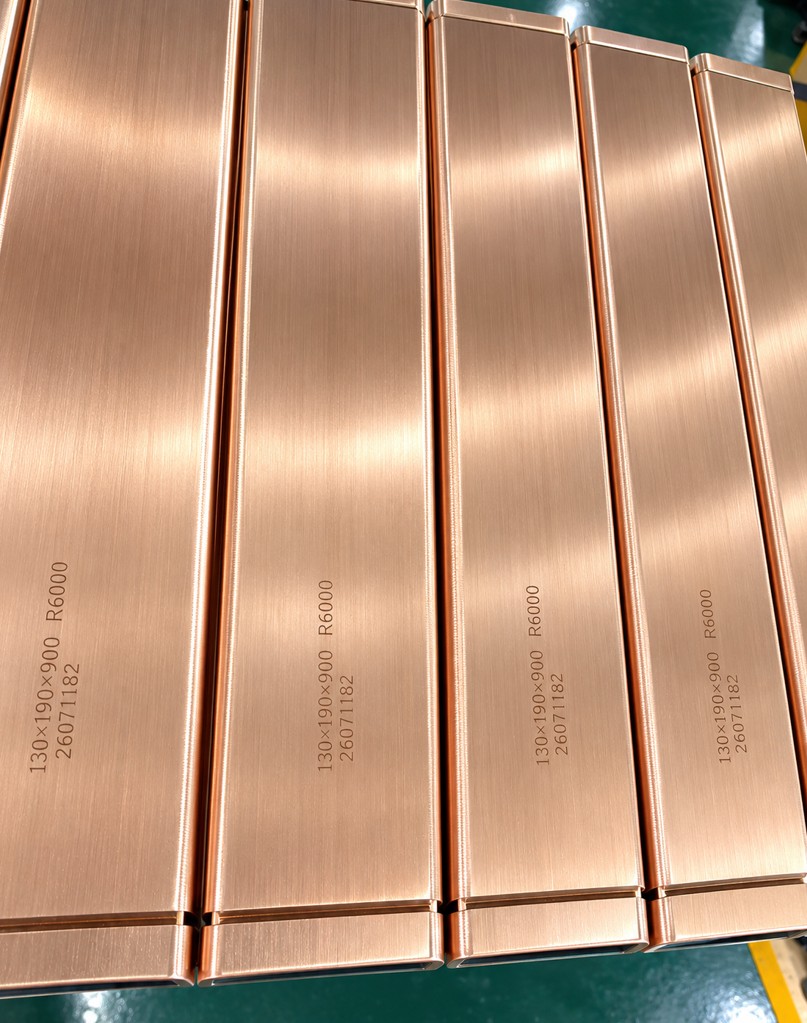
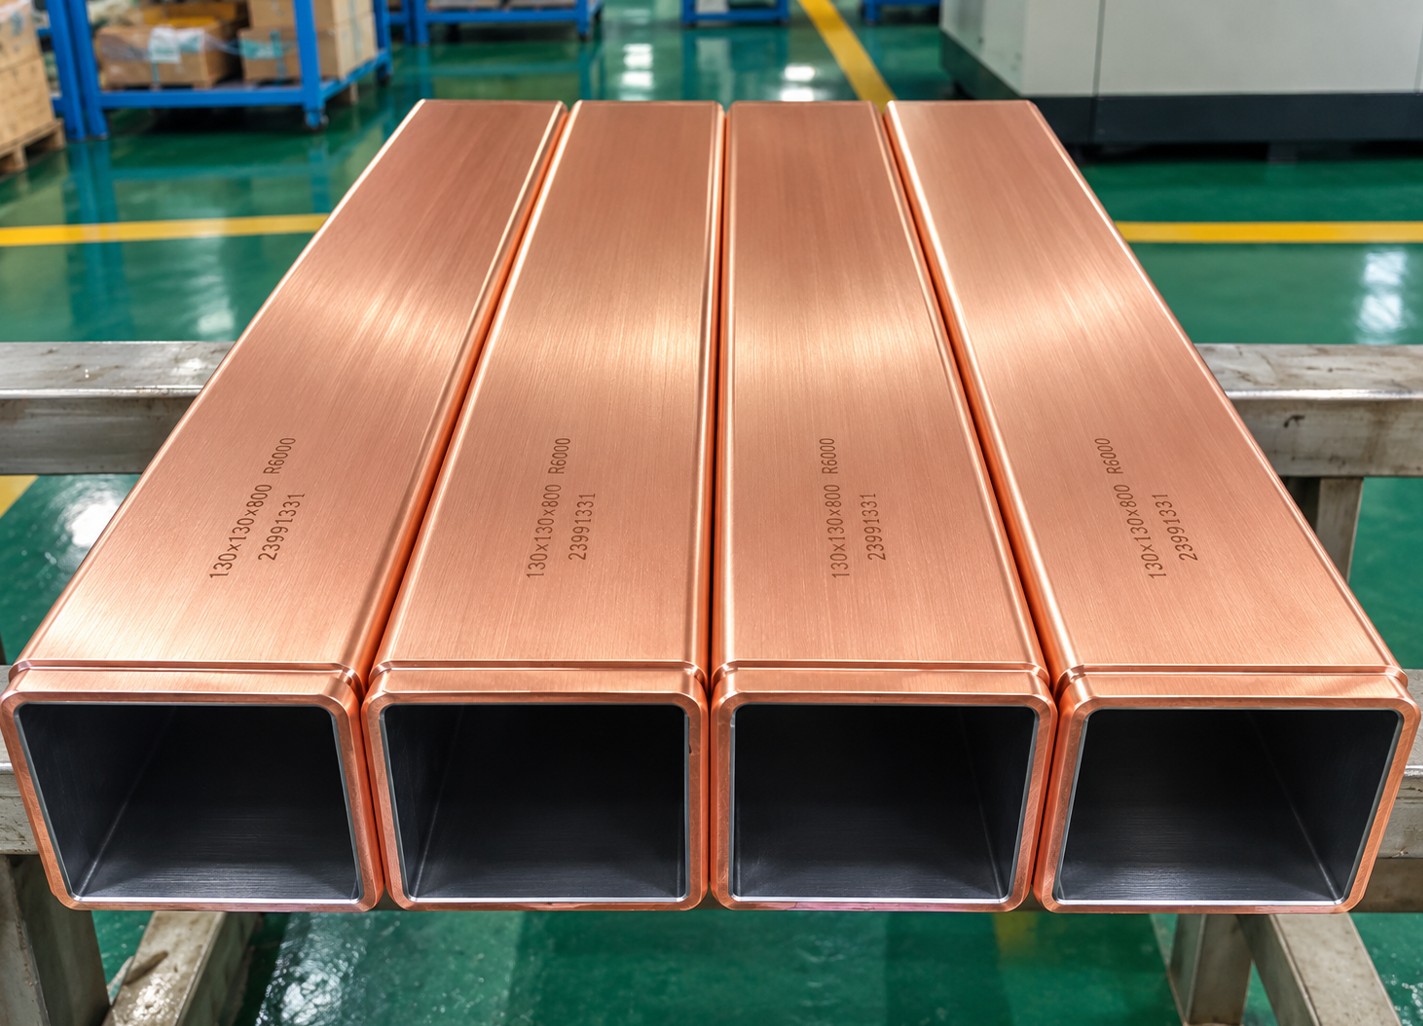
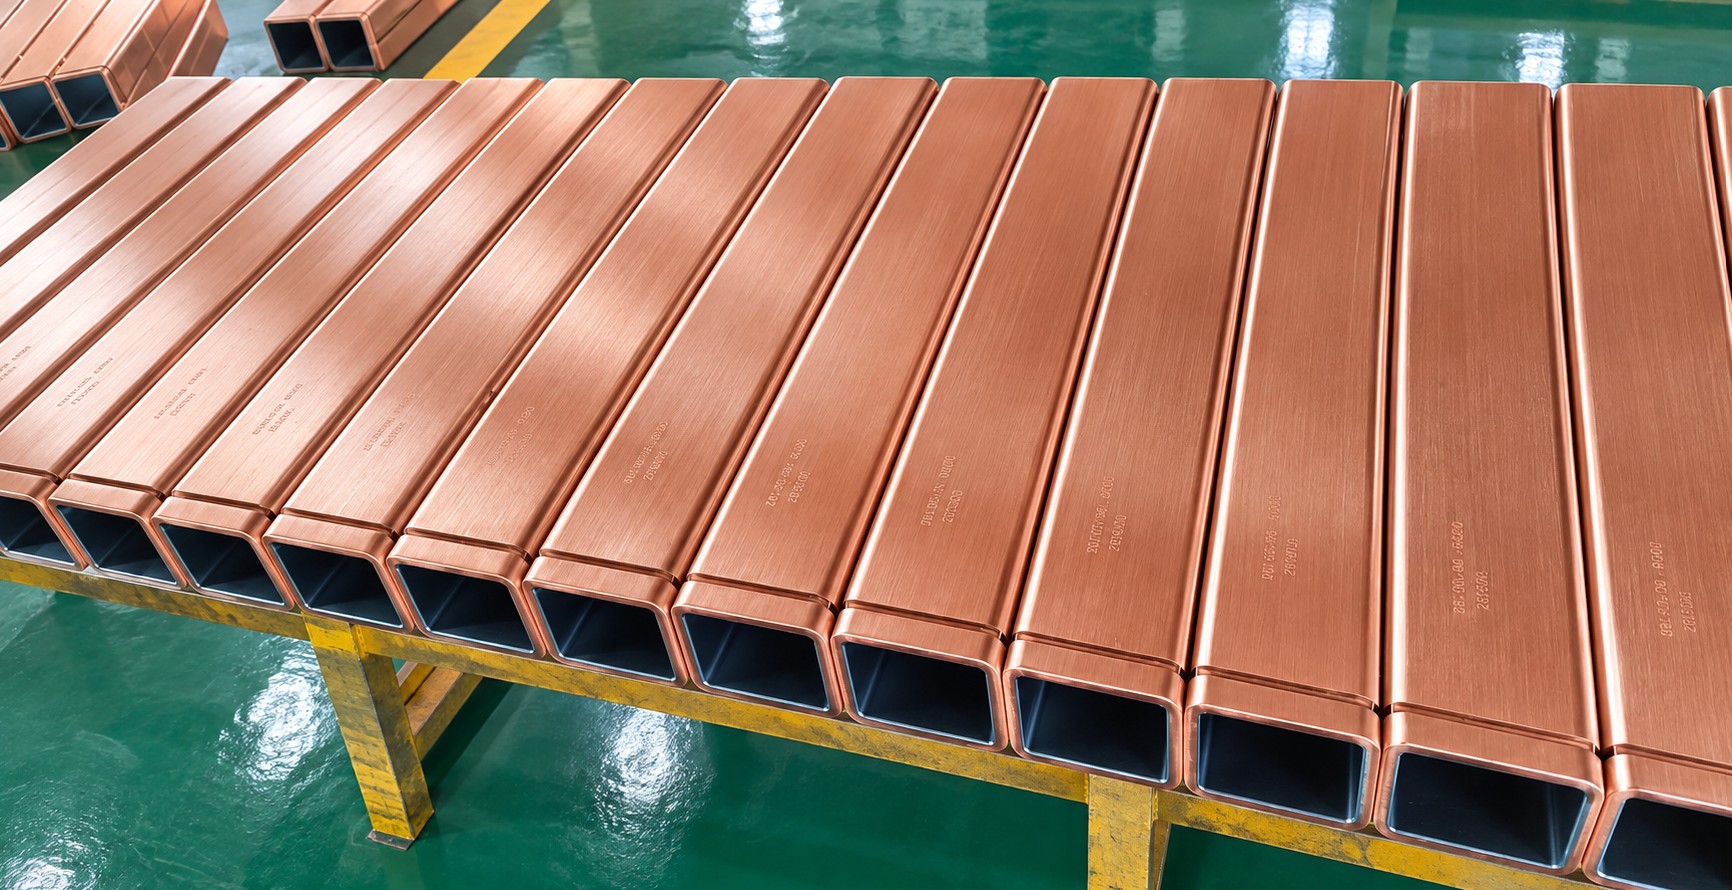
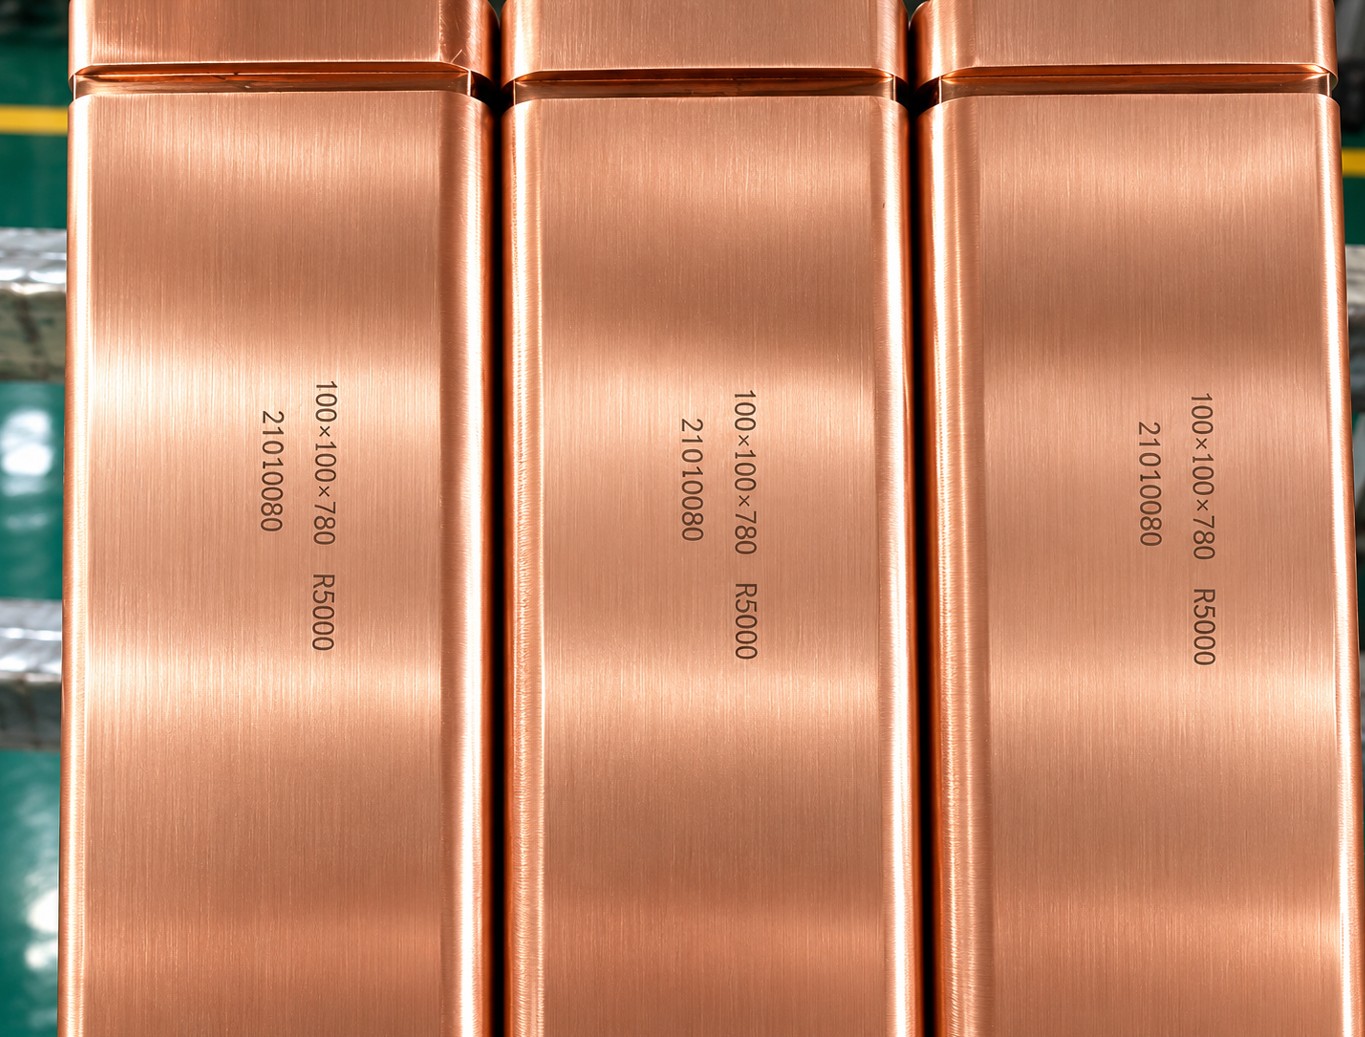
R3000 to R15000, square 70–200 mm, rectangular up to 150 × 520 mm, round Ø90–Ø500 mm. See the full tables below, then send us your drawing or the old tube's markings.
Request a quoteNamed by the cast section and tube form. All types are supplied with single, double, multi or parabolic taper according to the caster.
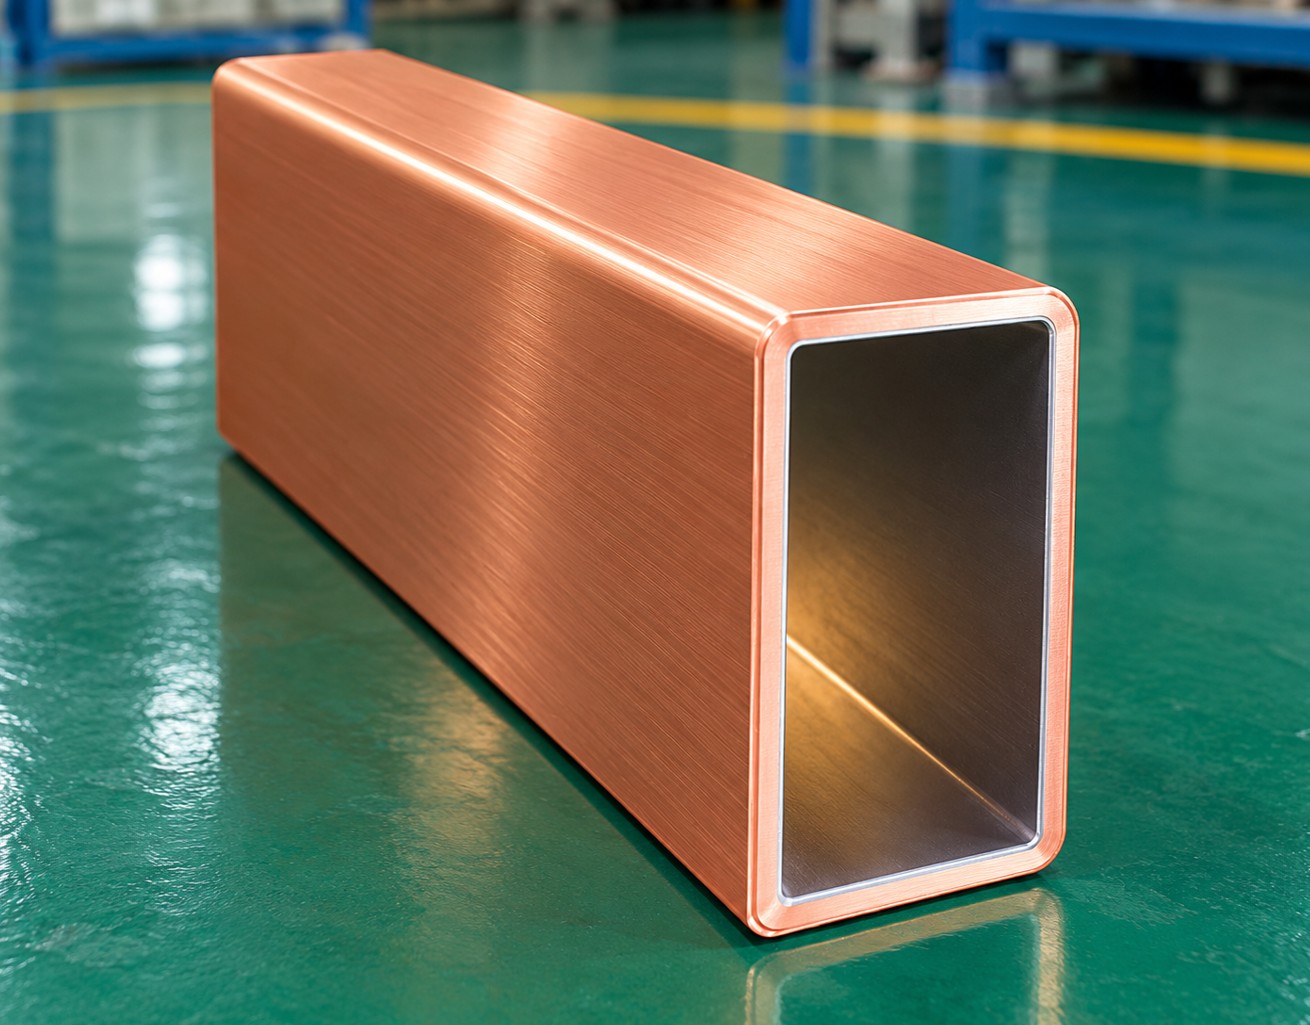
Bloom and beam-blank casters, 120×220 up to 150×520 mm
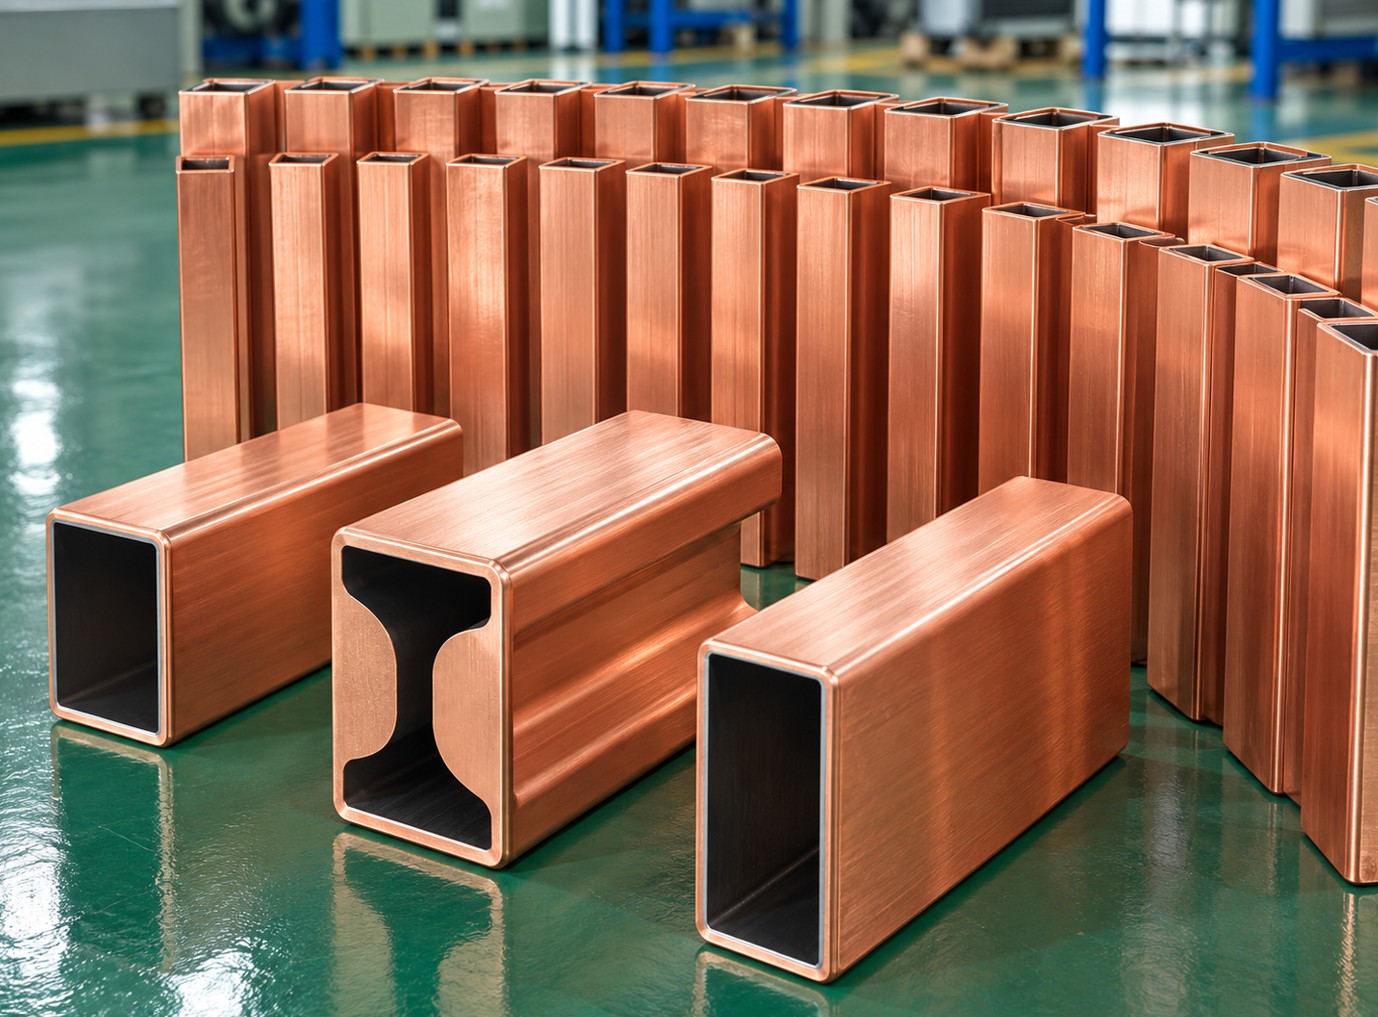
One-piece tube type mould, the standard for billet casters
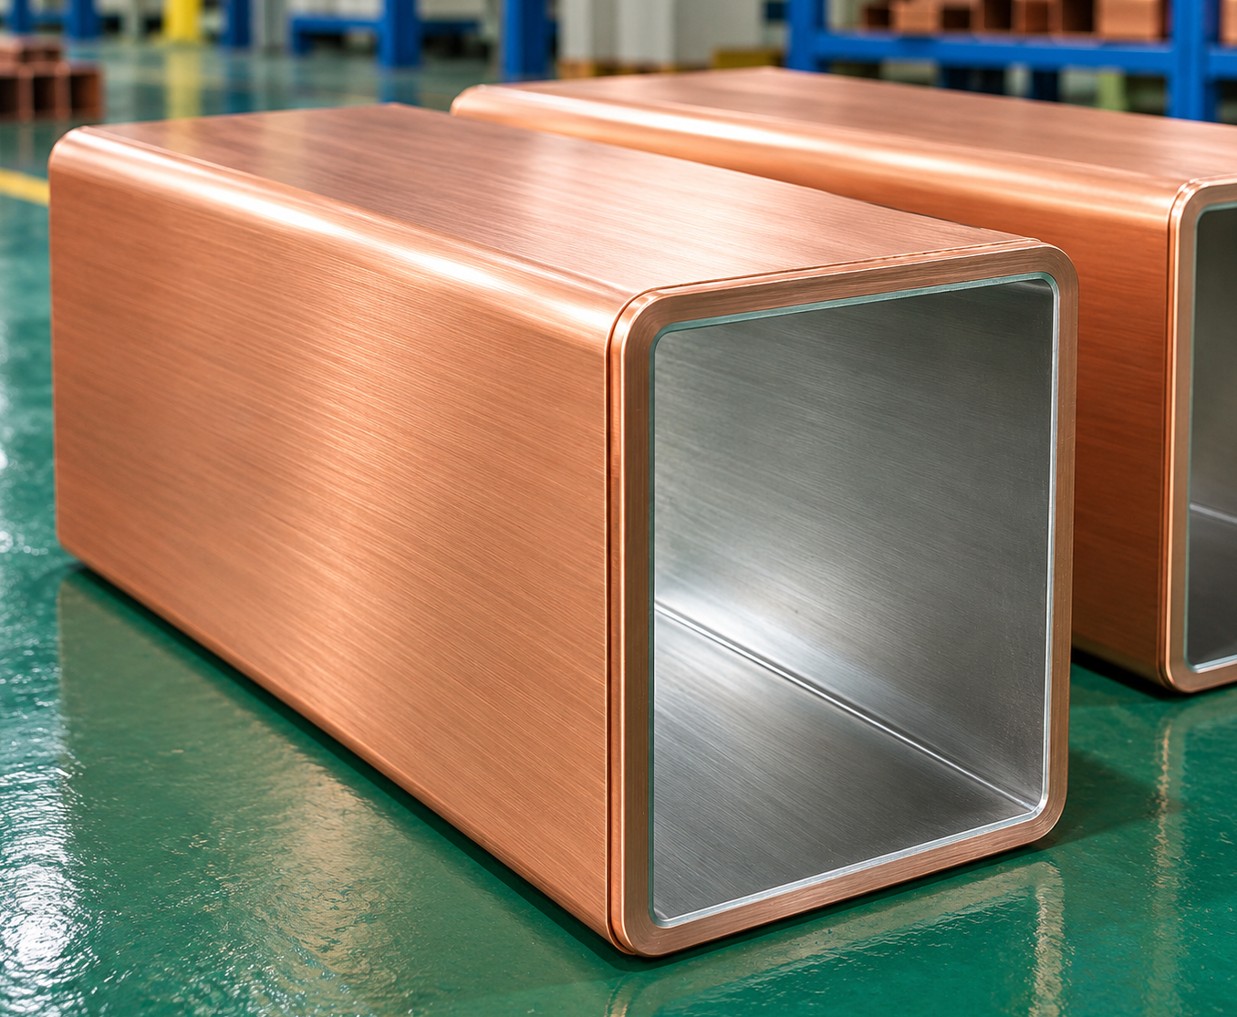
70×70 to 200×200 mm, the most common billet section
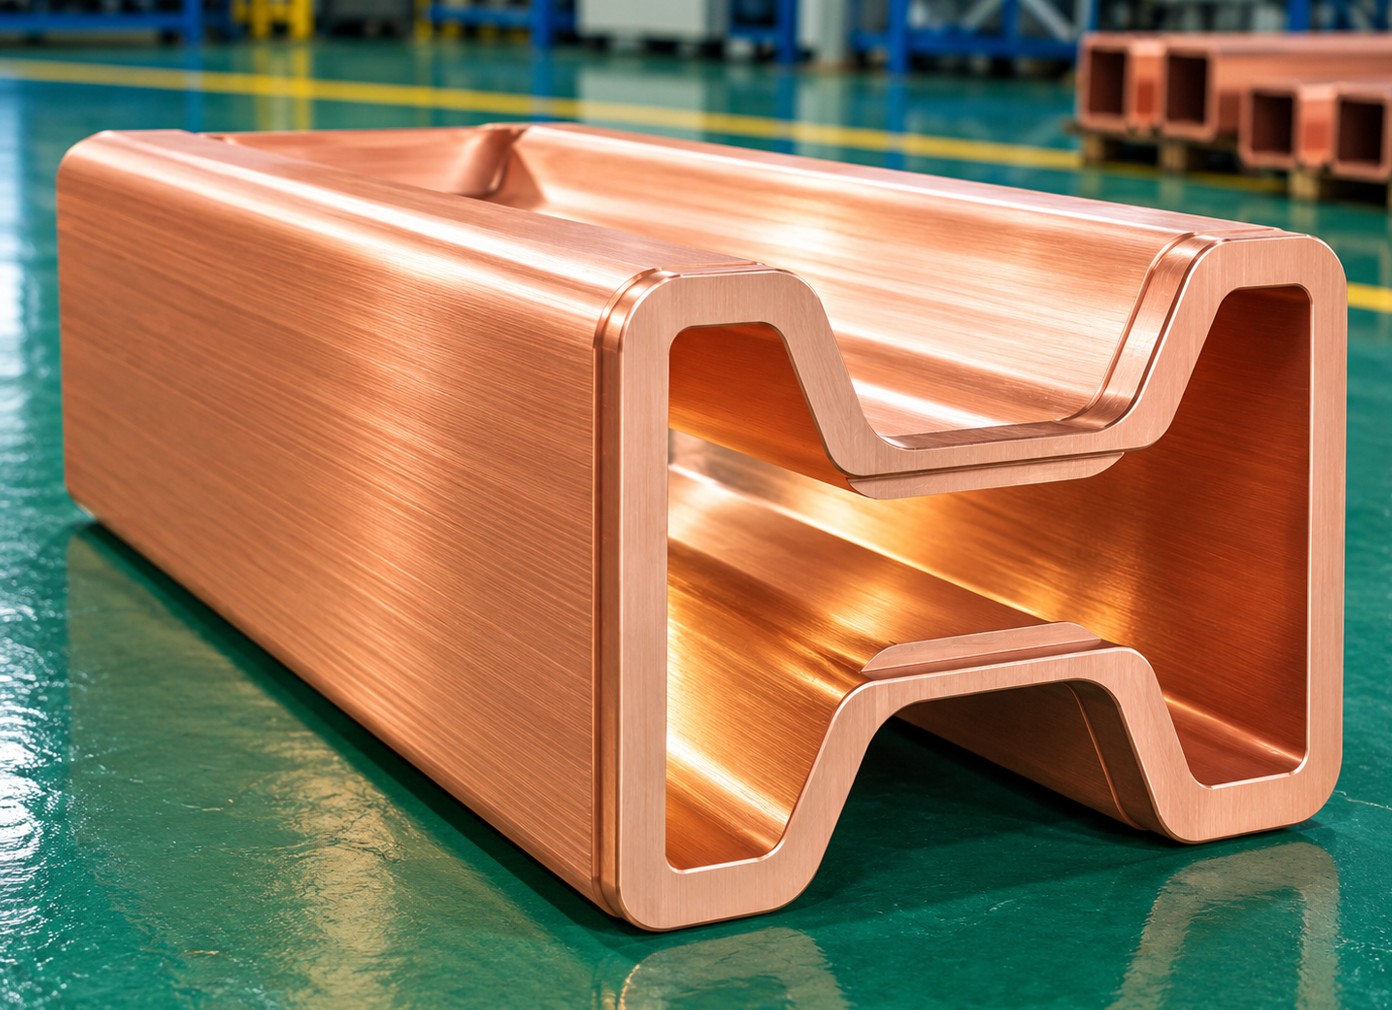
Beam blank (dog-bone) sections for structural steel casters
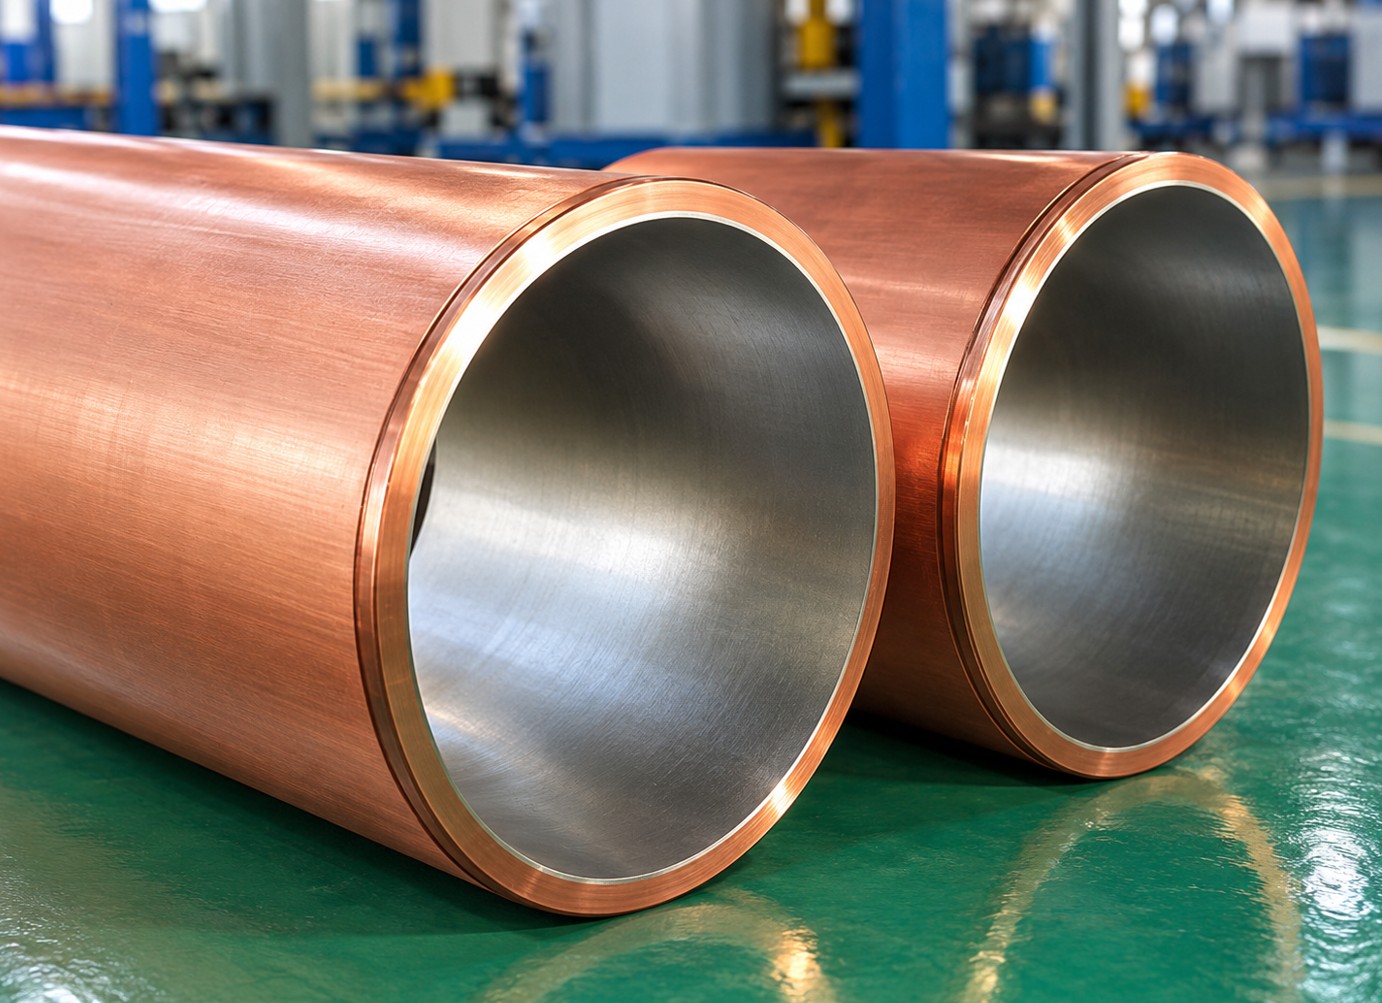
Ø90 to Ø500 mm for round billet and pipe-grade casting
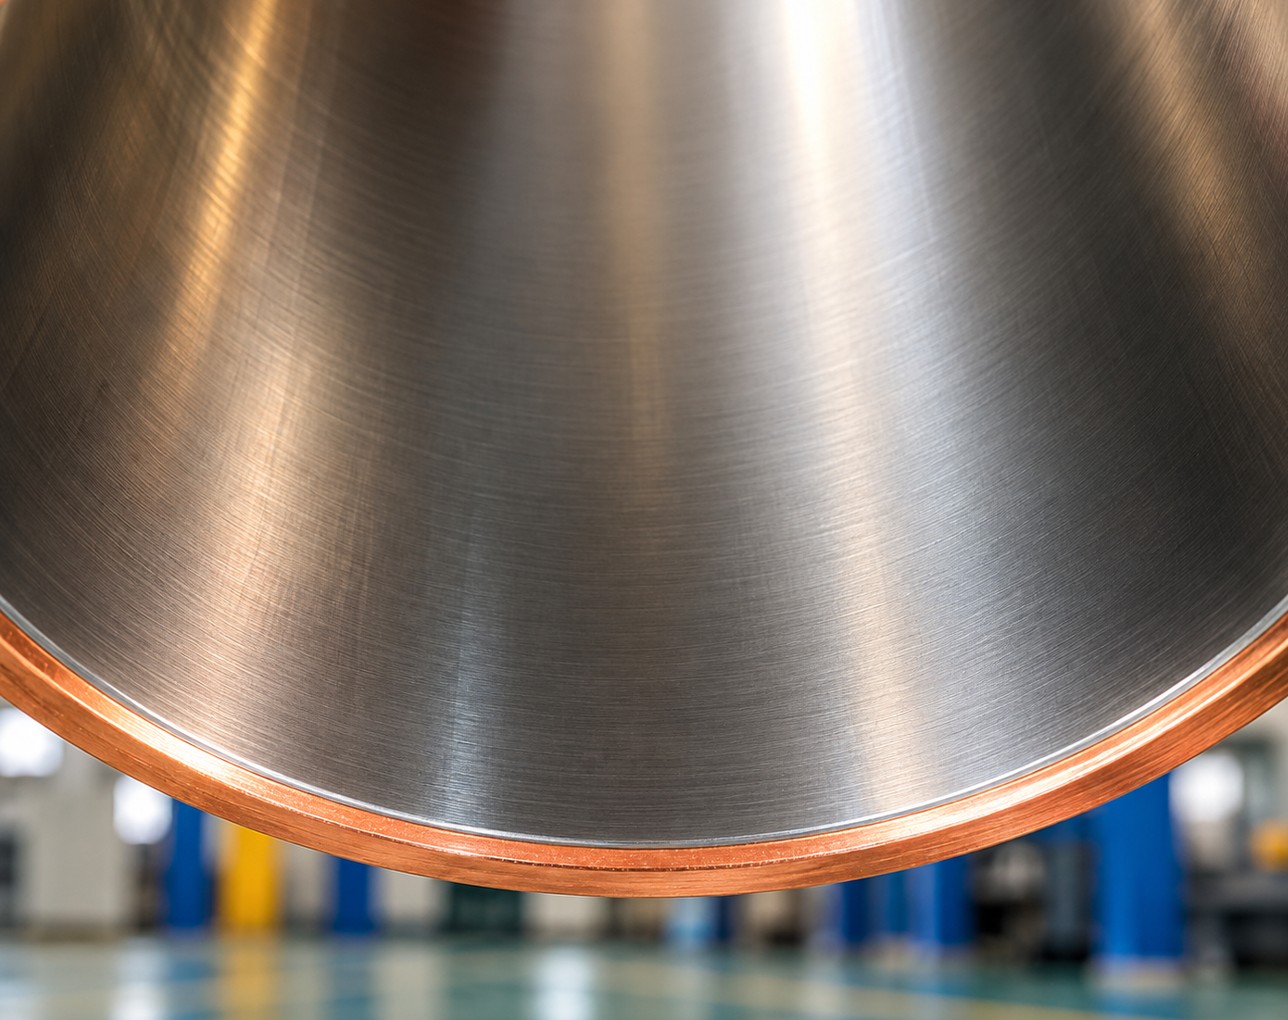
Hard chrome or Ni-Cr plated bore, polished, taper checked
Cast section, casting machine radius and product length for the tubes we manufacture. Radius and length are ranges: the exact value follows your caster drawing.
| Cast section (mm) | Casting machine radius R (mm) | Product length L (mm) |
|---|---|---|
| 70×70 | R3000–5000 | L812–850 |
| 80×80 | R3000–5000 | L812–850 |
| 90×90 | R3000–6000 | L812–850 |
| 100×100 | R3000–6000 | L812–900 |
| 110×110 | R3000–6000 | L812–900 |
| 120×120 | R4000–8000 | L800–900 |
| 130×130 | R4000–8000 | L812–900 |
| 135×135 | R4000–8000 | L812–900 |
| Cast section (mm) | Casting machine radius R (mm) | Product length L (mm) |
|---|---|---|
| 140×140 | R4000–8000 | L812–900 |
| 150×150 | R4000–8000 | L812–900 |
| 160×160 | R6000–9000 | L812–900 |
| 175×175 | R6000–9000 | L812–900 |
| 180×180 | R6000–9000 | L812–900 |
| 195×195 | R6000–10000 | L812–900 |
| 200×200 | R6000–10000 | L812–900 |
| Cast section (mm) | Casting machine radius R (mm) | Product length L (mm) |
|---|---|---|
| 150×140 | R6000–8000 | L800–900 |
| 150×155 | R6000–8000 | L800–900 |
| 180×240 | R8000–9000 | L900 |
| 165×225 | R8000–9000 | L900 |
| 160×220 | R6000–9000 | L900 |
| 120×220 | R6000–9000 | L900 |
| 165×280 | R9000–10000 | L900 |
| 175×225 | R6000–9000 | L900 |
| 130×285 | R6500–8000 | L900 |
| Cast section (mm) | Casting machine radius R (mm) | Product length L (mm) |
|---|---|---|
| 155×185 | R6000–8000 | L900 |
| 140×155 | R6000–8000 | L900 |
| 155×165 | R6000–8000 | L900 |
| 150×245 | R6000–8000 | L900 |
| 165×285 | R6000–10000 | L900 |
| 120×225 | R6000–10000 | L900 |
| 130×225 | R6000–10000 | L900 |
| 150×520 | R6000–10000 | L900 |
| 150×490 | R6000–10000 | L900 |
| Cast section (mm) | Casting machine radius R (mm) | Product length L (mm) |
|---|---|---|
| Ø90 | R3000–5000 | L812–850 |
| Ø100 | R3000–6000 | L812–850 |
| Ø105 | R5000–6000 | L812–900 |
| Ø110 | R6000 | L810–900 |
| Ø120 | R5250–8000 | L812–900 |
| Ø130 | R5250–8000 | L812–900 |
| Ø140 | R5250–8000 | L812–900 |
| Ø150 | R5250–8000 | L812–900 |
| Ø160 | R6000–9000 | L812–900 |
| Ø180 | R6000–10000 | L812–900 |
| Ø190 | R6000–10000 | L812–900 |
| Ø200 | R6000–10000 | L812–900 |
| Cast section (mm) | Casting machine radius R (mm) | Product length L (mm) |
|---|---|---|
| Ø210 | R6000–10000 | L812–900 |
| Ø220 | R6000–10000 | L812–900 |
| Ø230 | R6000–10000 | L812–900 |
| Ø280 | R6000–10000 | L812–900 |
| Ø310 | R6000–15000 | L812–900 |
| Ø320 | R6000–15000 | L812–900 |
| Ø330 | R6000–15000 | L812–900 |
| Ø340 | R6000–15000 | L812–900 |
| Ø350 | R6000–15000 | L812–900 |
| Ø400 | R6000–15000 | L812–900 |
| Ø450 | R6000–15000 | L812–900 |
| Ø500 | R6000–15000 | L812–900 |
Wall thickness 8–20 mm depending on section. Materials: Cu-DHP (TP2), CuAg (0.08–0.12 % Ag), CuCrZr. Inner plating: hard chrome 0.08–0.12 mm or nickel-chrome. Sections not listed are also accepted. Download or print this page for your maintenance file.
Every tube is measured on a CMM against the drawing; the report ships with the tube.
Hard chrome 0.08–0.12 mm, uniform along the full length, polished to reduce friction and sticker breakouts.
Cu-DHP for standard speed, CuAg for high speed, CuCrZr for long campaigns. We advise on the grade.
Used tubes with worn plating can be re-machined and re-plated instead of replaced.
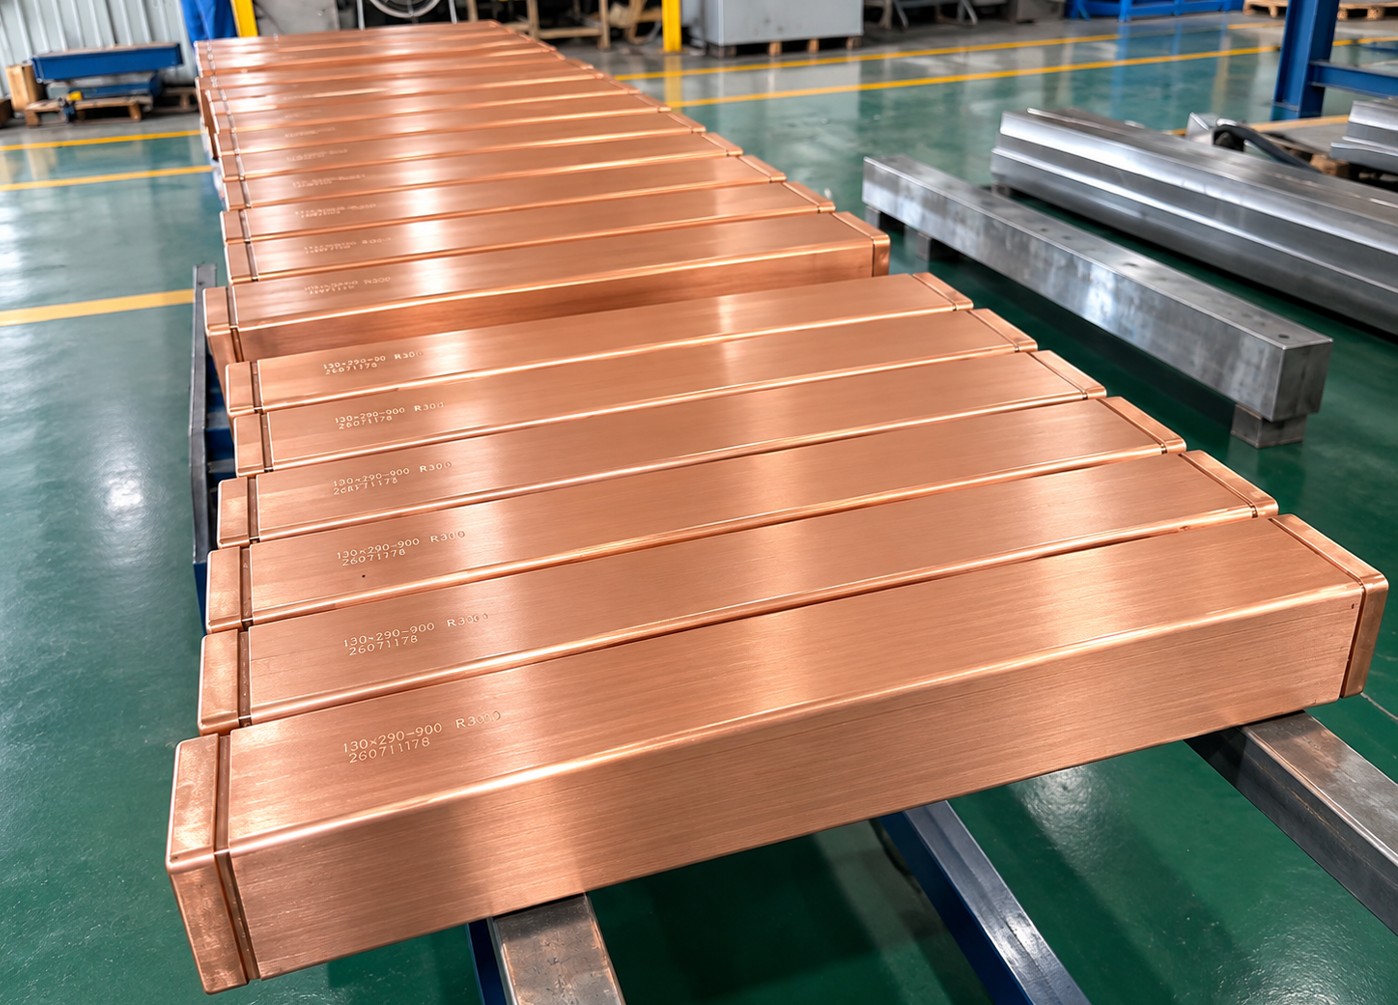
Send the tube drawing, the caster manufacturer's mould specification or a photo of the marking on your old tube (for example "150×150×900 R6000"). We confirm taper, wall thickness, water slot and plating before quoting.
Fill in the specification you need. Drawings can be sent to sales@coppermouldtube.com or by WhatsApp. Our sales engineer replies within one working day.